Manufacturing setup
From intake to dispatch, under one roof.
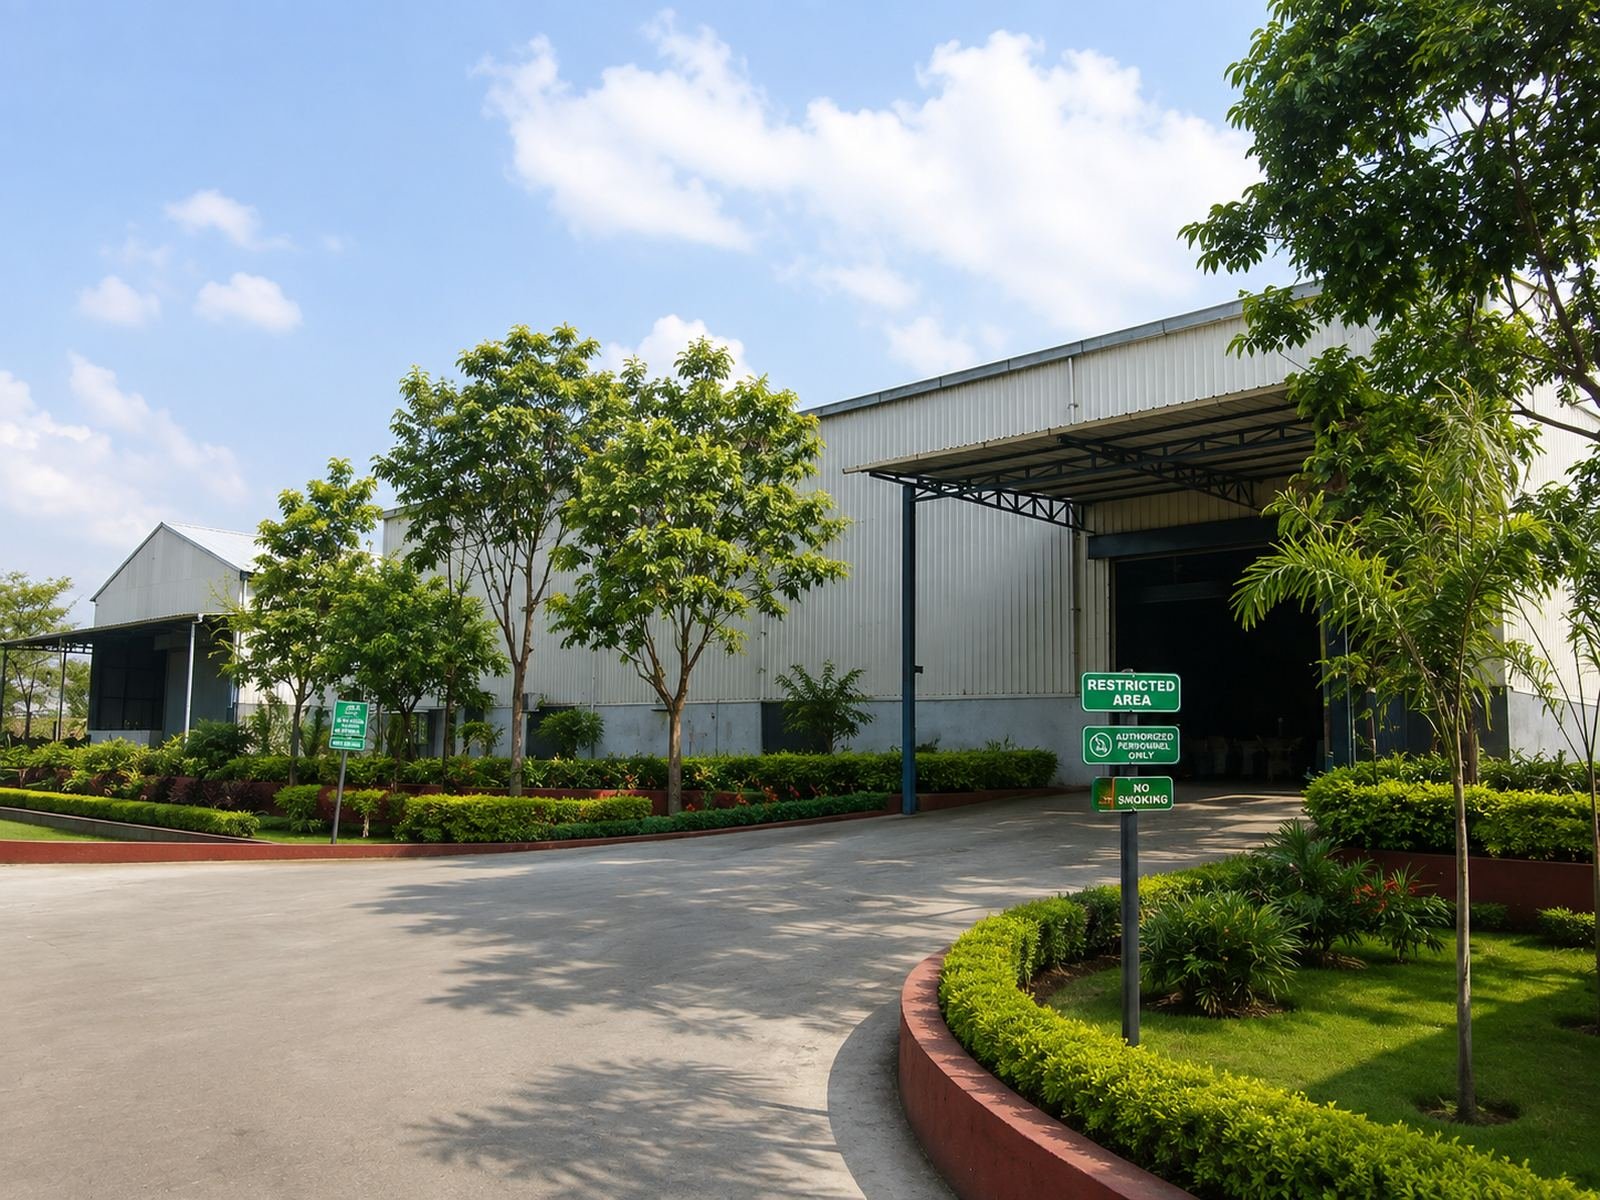
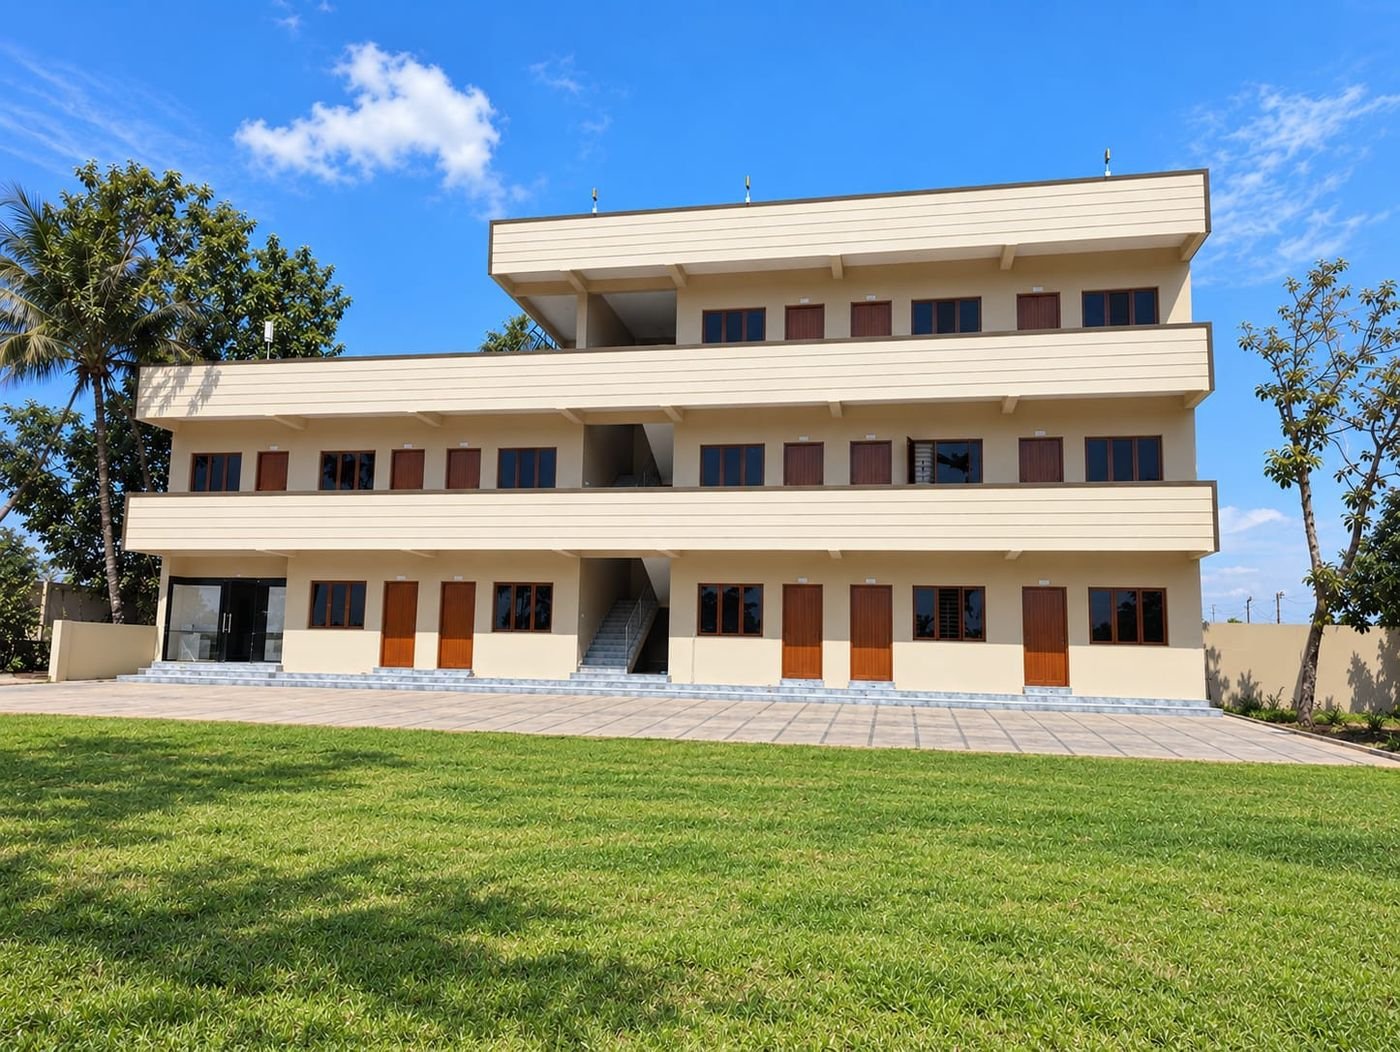
A purpose-built rendering facility at Hunasanalu, Nanjangud Taluk, producing 30 MT of poultry meal and 7 MT of poultry fat per day on imported, industry-grade equipment — with in-house laboratory control and on-site effluent treatment on a single controlled site.
The plant
Purpose-built, and run to plan.
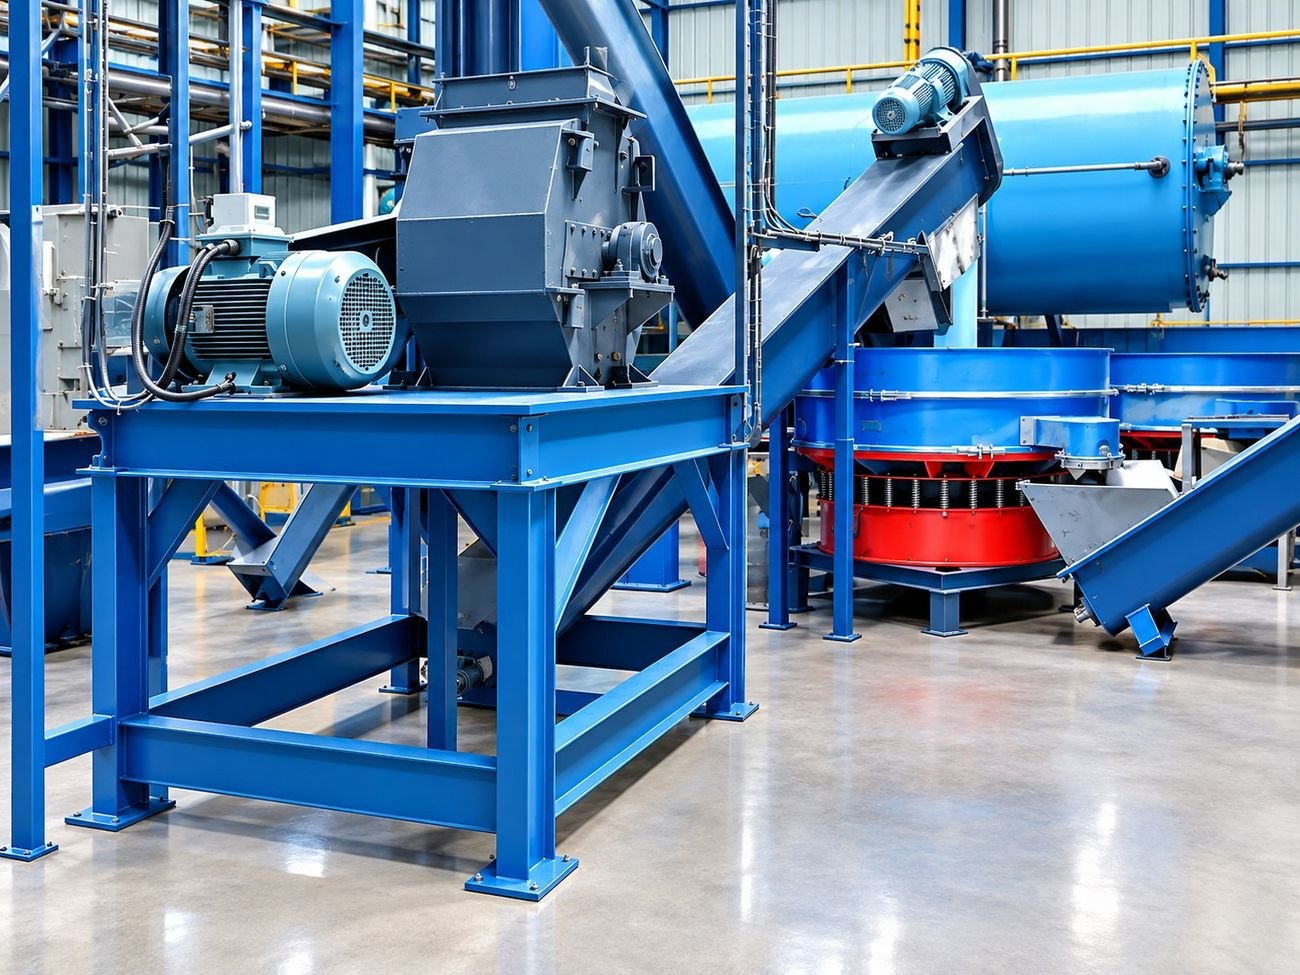
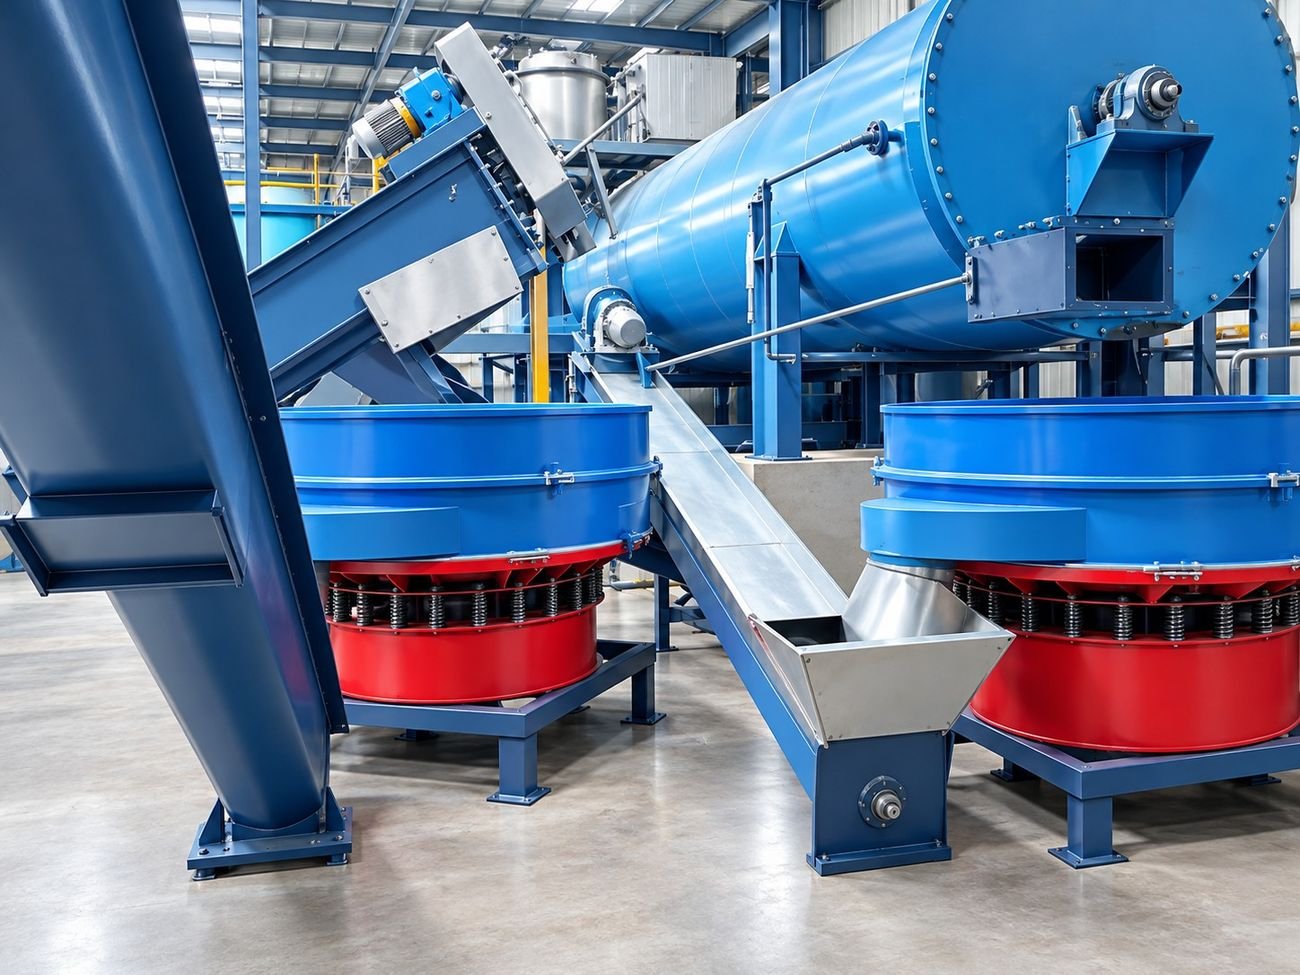
The site is laid out so material moves one way — from a segregated raw material reception area, through thermal processing, to a clean finished-goods zone. Personnel, equipment and material flows are separated to keep processed product away from incoming raw material at every point.
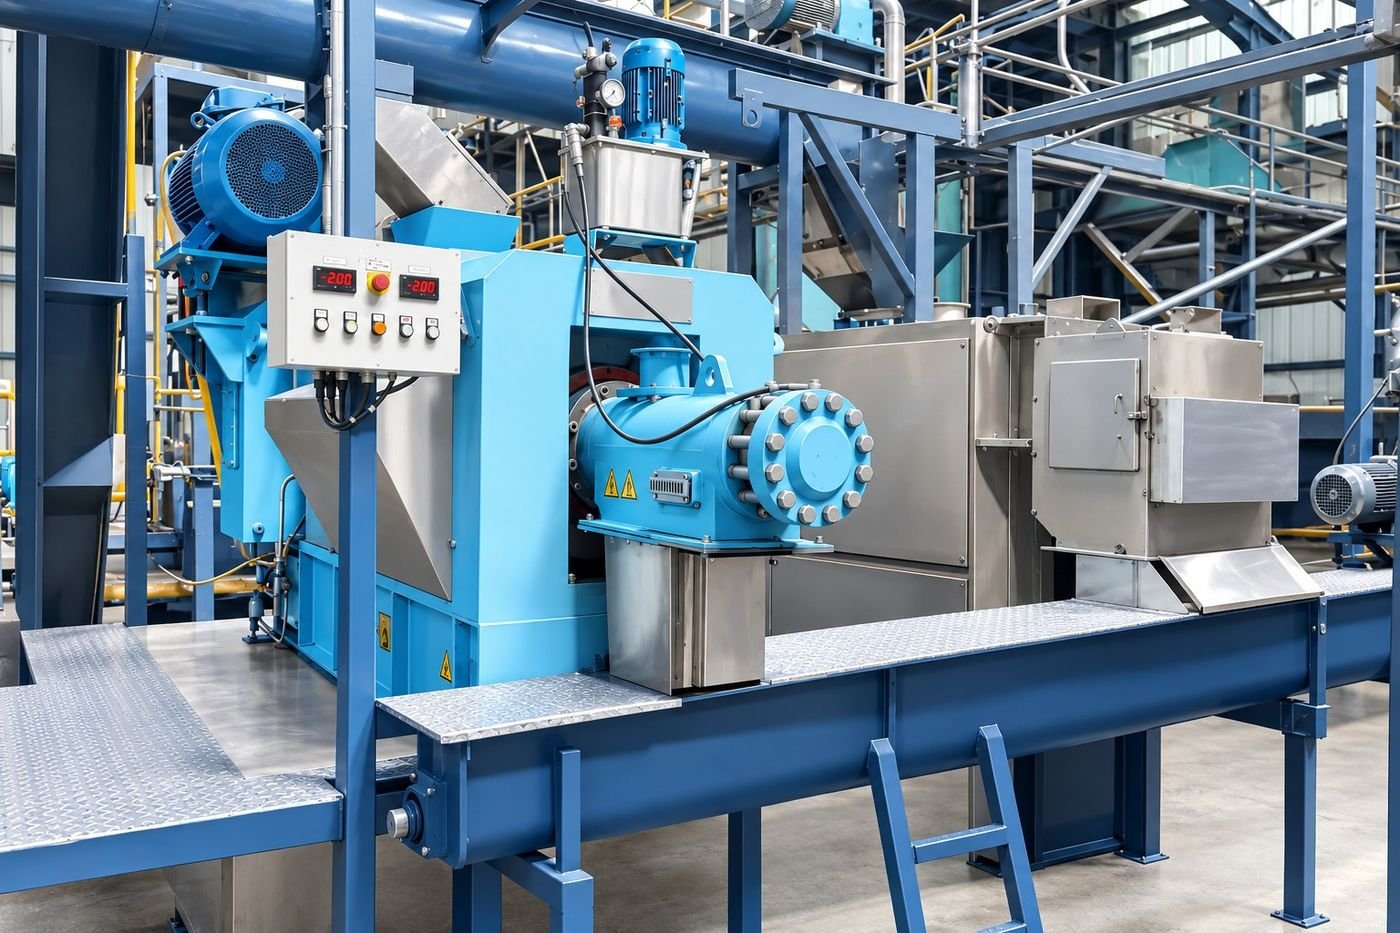
The line is built on imported, industry-grade equipment — Haarslev continuous cookers and screw press systems, and an Alfa Laval decanter centrifuge for fat clarification. Utilities, effluent treatment and the quality laboratory sit on the same site, so a batch can be produced, tested and released without leaving our control.
Process flow · six stages
How a consignment is made.
Raw material reception & segregation
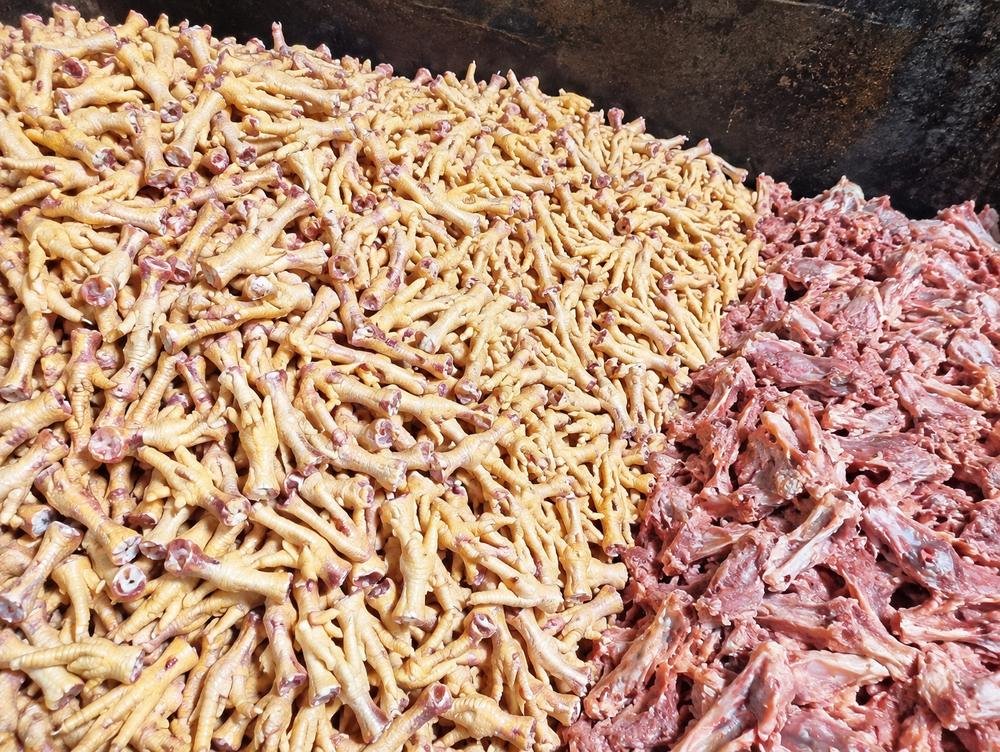
Poultry by-products are received from approved and evaluated suppliers into a dedicated, hygienically maintained intake bay. Each inbound load is checked for freshness and condition, recorded against its source, and segregated by category so that meal with feather and meal without feather are produced from correctly separated streams.
Thermal rendering & feather hydrolysis
Material is processed through Haarslev continuous cookers under a controlled time–temperature profile. For PML, feather is hydrolysed under controlled conditions so that keratin protein becomes digestible rather than inert. The profile is set to maximise nutrient recovery while protecting protein quality and keeping the meal free-flowing and stable.
Screw pressing, decanting & fat recovery
Cooked material passes through Haarslev screw press systems to separate the lipid fraction from the protein solids. Recovered fat is clarified on an Alfa Laval decanter centrifuge, held under conditions that protect it from oxidation, and filled out as poultry fat for dispatch. The press cake continues on to milling.
Milling, screening & contamination control
Press cake is milled to the required particle size and screened. Foreign-material prevention controls — including magnetic separation and screening — operate at this stage to protect against contamination before the product reaches finished goods.
Laboratory release, bagging & dispatch
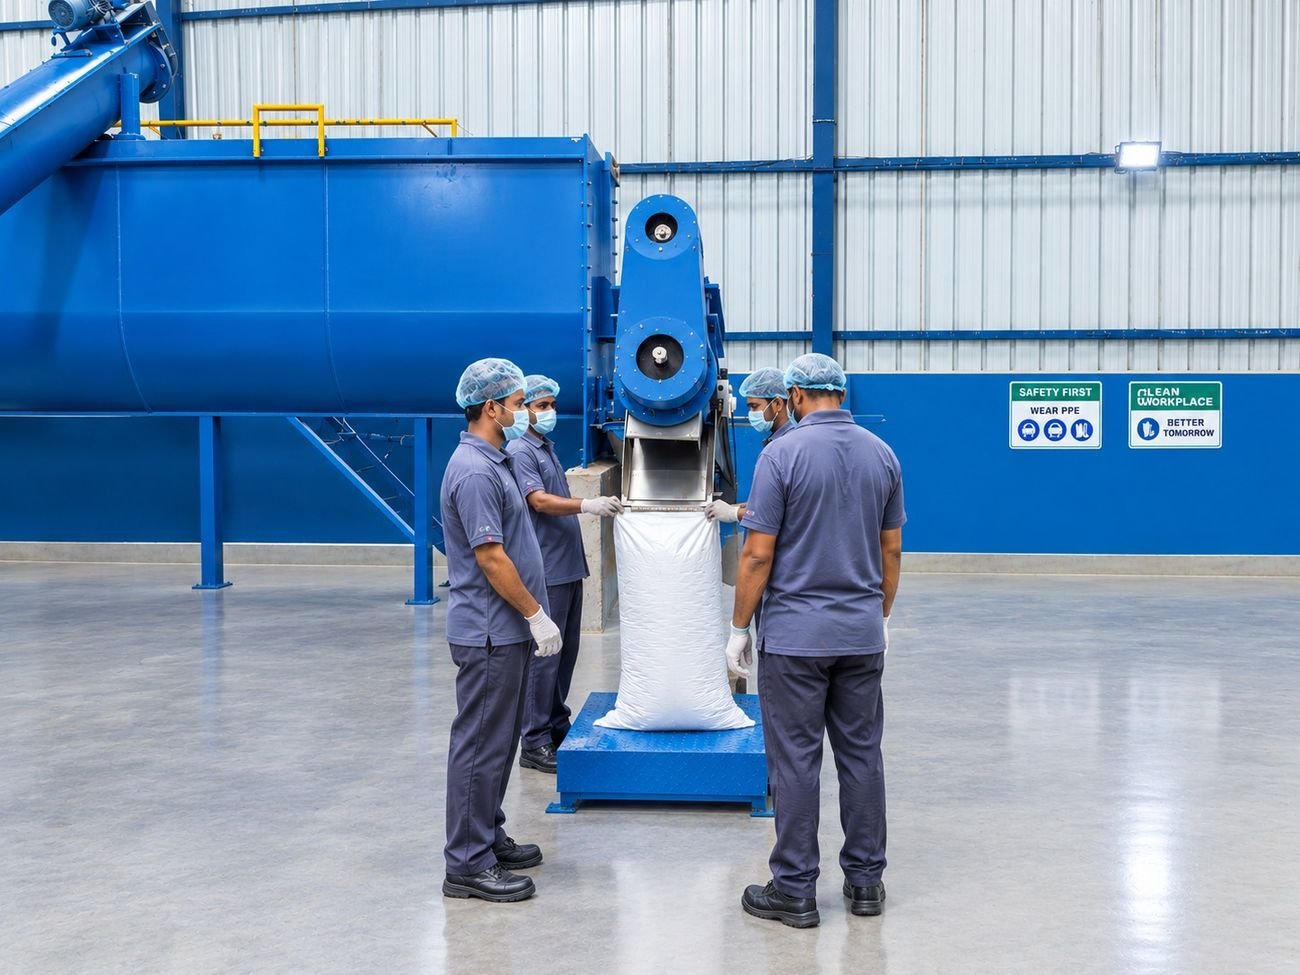
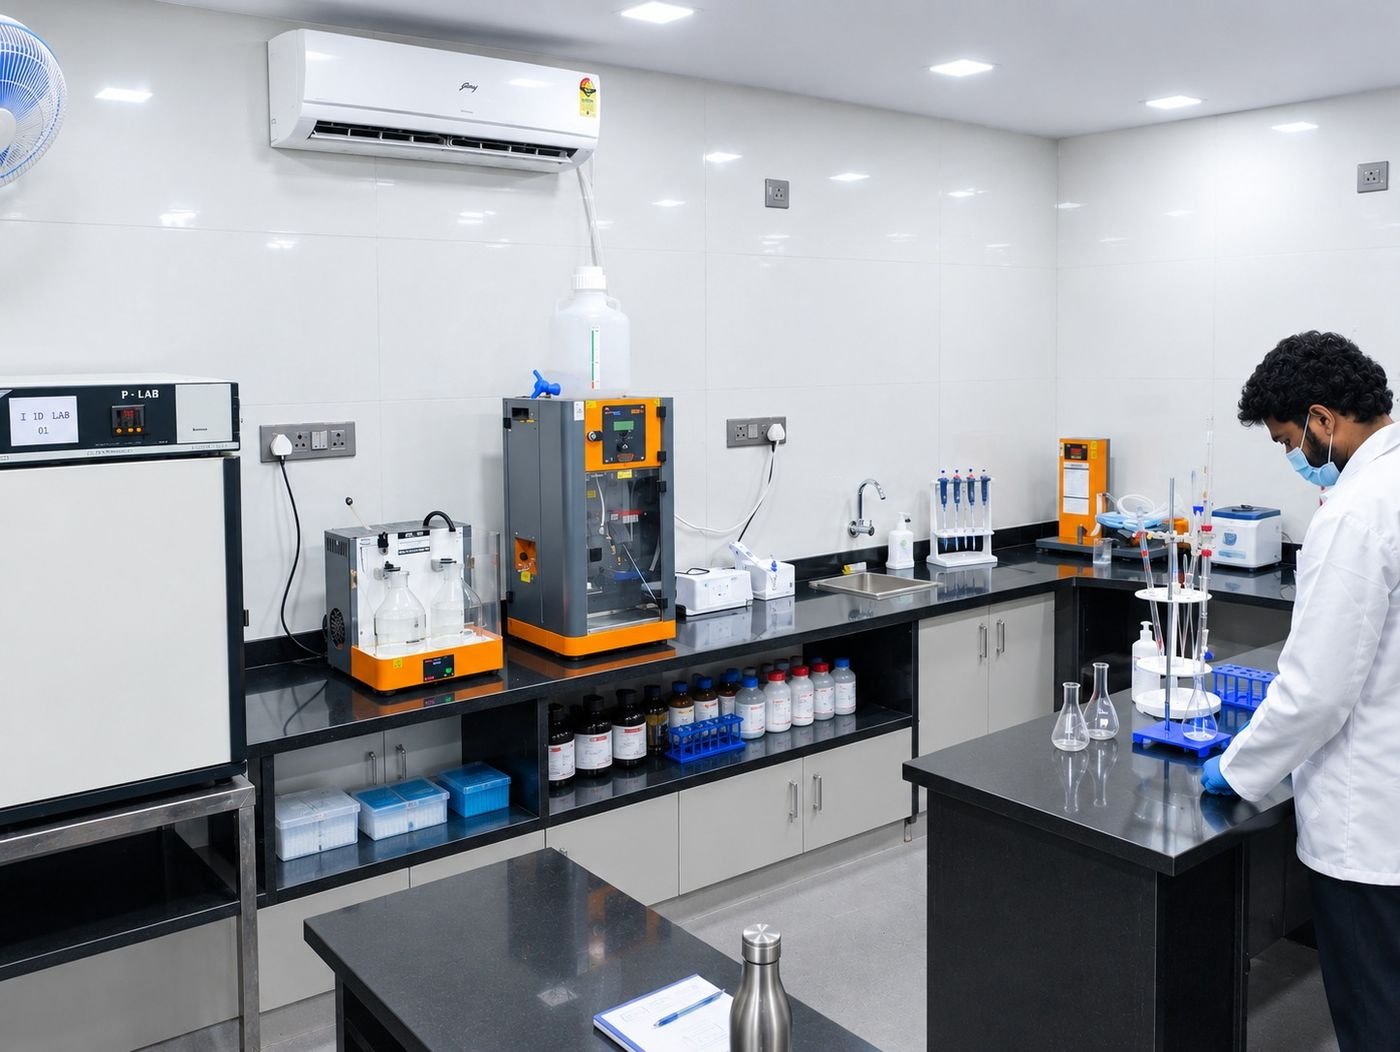
Every batch is sampled and tested in-house for protein, fat, moisture, ash and related parameters before release. Released material is bagged in 40 kg each for PML and 50 kg each for PMFL, coded with batch number and manufacturing date, stored in a cool, dry finished-goods area and dispatched with full traceability back to intake.
Supporting infrastructure
What keeps the line running.
- Haarslev continuous cookers — controlled time–temperature thermal rendering, 30 MT meal per day
- Haarslev screw press systems — mechanical separation of fat from protein solids
- Alfa Laval decanter centrifuge — clarification of recovered poultry fat, 7 MT per day
- Quality laboratory — Kjeldahl nitrogen distillation, digestion block, analytical balance, moisture and fat analysis
- Effluent treatment plant — on-site ETP treating all process wastewater
- Odour & emission control — controlled air emission systems including odour and ammonia management
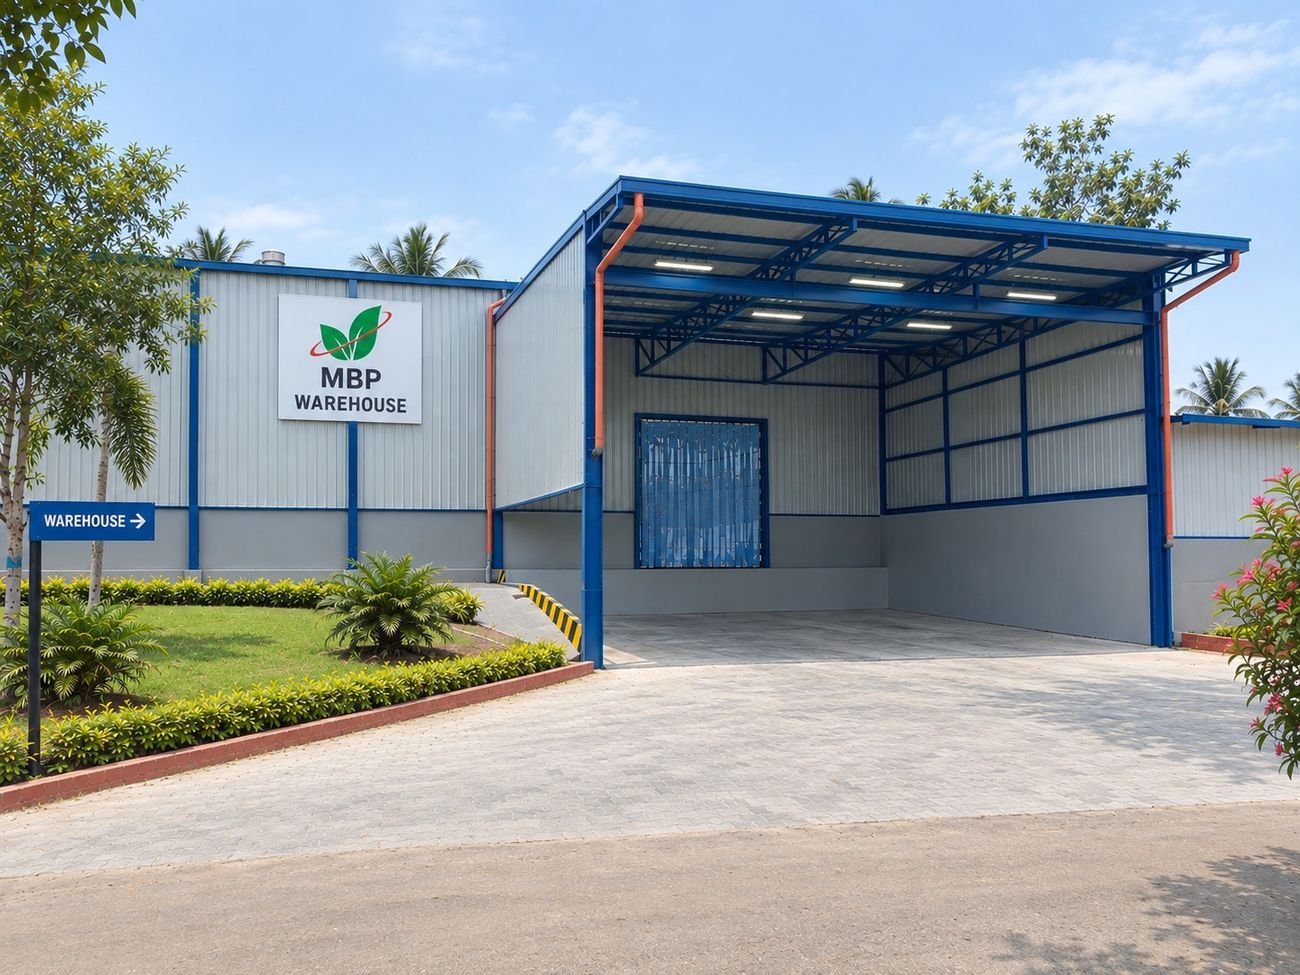
- Finished goods storage — cool, dry, hygienic warehousing prior to dispatch
- Continuous operation — the plant runs 24 × 7
Facility at a glance
Inside the plant.
Want to audit the plant?
We welcome customer and third-party audits. Get in touch and we will arrange a facility visit and share our documentation pack in advance.